
High-speed thin-strip leveling
U-Type High-Speed Leveler for Transformer & Motor Cores
Straighten thin coil strip and buffer it in a U-shaped loop before high-speed feeding. The HENLI JMU series supports EI/UI laminations, transformer cores, motor cores and other thin-strip stamping applications.

Why the U-loop matters
A Material Reserve Between Leveling and Intermittent Feeding
After the strip is leveled, it forms a U-shaped loop before downstream feeding. The buffer helps accommodate changes in strip demand as the feeder advances material through repeated press cycles.

U-Shaped Buffer Path
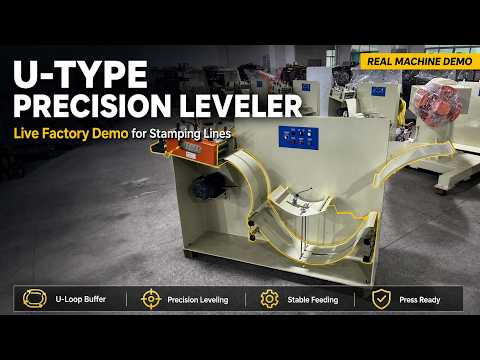
The pictured unit is marked TUS-400. Its U-shaped path illustrates strip buffering between leveling and feeding; check the setup for the selected material.

Machine Frame and Loop Arrangement
The workshop units show the U-loop body and leveling section. Review the footprint, working height and access when planning an installation.
Roller setup and loop sensing
Prepare the Strip and Coordinate Its Supply
Required flatness, material condition and the downstream process guide the setup. The loop control coordinates supply during normal production.
15 Leveling Rollers
The JMU table lists Ø32 mm rollers with 7 upper and 8 lower. The 2 pinch rolls provide a separate adjustable-pressure feeding function.
Four-Point Vertical Adjustment
Set roller engagement and pinch pressure for the actual strip. Check the resulting flatness and surface condition when establishing the working setup.
Photoelectric Sensing and Speed Control
Photoelectric sensing monitors the loop condition, with frequency-controlled speed regulation. Confirm the control modes and interfaces for the supplied JMU configuration.
Line integration
From Coil Pay-Off to High-Speed Stamping
The U-Type leveler normally works between the decoiler and the downstream feeder. Match the full equipment set to the coil, die, feed pitch and press speed.
Support and Unwind
Select coil handling for the weight, I.D./O.D. and changeover requirements. Review double-head decoilers.
Prepare and Buffer
Straighten the strip and maintain a suitable U-loop reserve before feeding.
Control the Feed Pitch
Match the feeding interval and die pitch. Review high-speed gear feeders.
Coordinate the Cycle
Confirm the press rhythm, material demand, working height and control interfaces for the installation.

Coil Pay-Off and Press-Line Overview
The installation shows the relationship between coil handling, U-Type leveling and high-speed stamping equipment.

Double-Head Decoiler and Leveler Arrangement
The workshop line groups coil handling and leveling equipment ahead of the presses. Plan equipment spacing and operator access for the chosen set.
Standard model selection
JMU-200, JMU-300 and JMU-400 Specifications
Use the actual width, thickness, material properties and required output to select the model. Confirm the minimum usable width, operating speed and line arrangement for the application.
| Specification | JMU-200 | JMU-300 | JMU-400 |
|---|---|---|---|
| Maximum strip width | 200 mm | 300 mm | 400 mm |
| Material thickness | 0.1–1.0 mm | 0.1–1.0 mm | 0.1–1.0 mm |
| Listed feeding speed | 45 m/min | 45 m/min | 45 m/min |
| Pinch rolls | 2 / adjustable pressure | 2 / adjustable pressure | 2 / adjustable pressure |
| Motor power | 1 HP | 1 HP | 2 HP |
| Leveling rollers | Ø32 mm, 7 upper / 8 lower | Ø32 mm, 7 upper / 8 lower | Ø32 mm, 7 upper / 8 lower |
| Adjustment method | 4-point vertical | 4-point vertical | 4-point vertical |
On a small screen, scroll the table sideways to compare all three models. The table covers JMU-200, JMU-300 and JMU-400. Photographs illustrate machine and line layouts; working capacity and controls follow the specification of the quoted machine.
Thin-strip applications
Transformer Laminations, Motor Cores and Similar Parts
Assess the electrical-steel or other strip grade, required flatness, surface condition and feeding cycle for the part you produce.
Transformer-Core Stamping
Prepare thin strip for repeat feeding and blanking of EI/UI lamination shapes.
Motor-Core Components
Coordinate the incoming strip condition with the high-speed feeder and lamination die.
Cutting and Blanking
Review the strip preparation and required result before cutting or stamping reactor components.
Suitable Thin-Strip Blanking
Confirm the material and selected JMU working range for other thin-strip stamping applications.
Workshop and installation
Plan the Equipment Around Your Existing Line
Check coil handling, machine position, transfer height and access for setup. A line drawing or site photographs help define the required equipment arrangement.

Decoiler, Transfer Area and Leveler
This workshop setup shows coil pay-off, a transfer table and the U-Type leveler. Check strip support and equipment spacing against the actual installation.

U-Type Units in the Workshop
The machine group shows the leveler bodies prepared for line projects. Specify the model and installation requirements for each production line.
Equipment selection
Compare the Strip Path, Process and Feeding Task
U-Type and S-Type are different thin-strip layouts. Compare their actual setup, available space and required result; the layout name alone does not establish better flatness or a particular storage length.
JMU U-Type Leveler
Review this route when thin-strip leveling and a U-loop buffer need to be integrated ahead of high-speed feeding.
S-Type High-Speed Leveler
Compare the S-shaped material route and line arrangement with the S-Type leveler. Confirm usable storage and output for the selected setup.
Precision Sheet & Coil Leveler
For material conditions, individual sheets or flat parts that call for precision leveling, review the appropriate SSL configuration.
Gear Feeder or NC Servo Feeder
Choose a gear feeder or NC servo feeder for the feed pitch, speed and press interface. A feeder controls advancement; the need for leveling is assessed separately.
For an existing feeding line, read when coil feeding requires a leveler.
Factory video
U-Type Leveler Operation and Factory Run
Review the machine arrangement and material loop in operation, then compare them with your strip and press requirements.
Quotation checklist
Send Your Strip and Press Data for JMU Selection
HENLI reviews the material, leveler, decoiler, feeder and press as a complete production setup.
FAQ


